
Bottle, Closure and Filling Interfaces
Filler Bottle Starvation: Find the Missing Infeed Condition
A filler waiting for bottles is not automatically an undersized blower. Distinguish usable-bottle supply, the physical infeed handoff and the machine's receiving permission before changing speed or buying capacity.
Decision focus
Where does usable bottle supply first stop, and which machine owns the resulting response?
01
Direct Answer
Confirm that the reported shortage is empty-bottle starvation rather than product-water, cap or utility loss. Compare the approved bottle format, actual infeed condition and time-aligned upstream/filler states. Map detection, supply request, agreed hold or stop response and restart permission; a machine-ready signal alone does not prove bottles are arriving.
Find the first loss of usable bottles before changing the line
Record the exact message, bottle format and affected time interval. The buyer's useful outcome is a starvation-response map identifying observation points, signal owners and recovery evidence, not a generic list of faster machines. Allot Tech can coordinate this scope review using supplied records and drawings; the project parties retain final engineering and quality authority.
Separate the shortage category from the alarm label
A general waiting or low-output message can hide different missing inputs. Ask the supplier what condition produces the displayed bottle-starved state and which observation point it represents. Product water unavailable, cap supply unavailable, a utility interruption and an empty-bottle gap require different evidence and owners. Preserve simultaneous states instead of treating the first message seen by an operator as the root cause. Compare a single approved bottle format and note whether the event followed a material, recipe or change-part revision. Do not convert an unverified alarm label into a feeder purchase decision.
Locate the first gap from bottle source to filler entry
Trace the agreed route from blower or other bottle source through transfer and filler reception. For the same interval, compare usable bottles leaving the source, their condition and orientation at each handoff, and the filler entry observation. A running blower does not establish continuous accepted delivery; rejected bottles, an interrupted transfer or incompatible format handling can break that link. Record controlled bottle/neck drawings and installed format references without prescribing a guide, airflow or speed adjustment. Qualified staff must investigate through approved guarded procedures; do not enter a moving conveyor or create a jam to collect evidence.
Write a receiving-condition and response contract
For each detecting state, state the source, signal meaning, receiver, agreed response, acknowledgement and restart permission. Distinguish normal shortage from equipment fault and define loss or contradiction of a signal as an open engineering question. The suppliers must agree any delay/filter basis against the actual detection and transfer arrangement; no universal delay belongs in the purchase brief. Machine ready, bottle available and permission to feed are not interchangeable promises. Include the fate of bottles already at the interface and who decides quality disposition after an uncertain event.
Compare evidence before accepting an upgrade
Hypothetical review: the blower remains in run while the filler reports starvation after a format change. Compare bottle acceptance and the first interrupted handoff, not only the two machines' nominal rates. Ask the responsible suppliers to link the format revision, event sequence and response map to an approved observation or acceptance plan. Record duration and frequency on a common interval and count accepted finished output separately from machine state time. An upgrade claim needs the same format and boundary before and after; a larger nameplate does not establish improvement. This is a review example, not a customer case or instruction to force a fault.
Evidence for a starvation-response review
- Exact alarm/state definition, observation point and supplier owner; distinguish bottles from water, caps and utilities.
- Approved bottle/neck drawings, samples, lot and format recipe or change-part revision for the observed interval.
- Time-aligned source, transfer and filler records showing the first delivery gap, plus any existing safely obtained observation.
- Signal/response map for request, available, receiving permission, shortage, fault and restart; unresolved items remain explicit.
- Common count/time boundary, affected bottles, quality-hold responsibility and a supplier-approved verification plan.
Project-specific engineering and quality review is required. This page does not set safe delay, pressure, airflow, conveyor speed or restart logic. Do not bypass safeguards or return held bottles without approved site procedures.
Continue the bottle-supply review
- Air conveyor to filler infeed — Check the physical receiving boundary and approved bottle basis.
- Bottle blowing and filling integration — Compare usable delivery with connected filling demand.
- Filler downstream-blocked response — Separate incoming shortage from an unavailable discharge path.
02
Position in the System
This guide isolates the named machine-to-machine decision and the project evidence needed to close it. It controls the boundary between Approved empty-container or closure supply and The connected handling, rinsing, filling or capping function. It does not select equipment models, publish unsupported performance values or replace project-specific engineering.
03
Buyer Inputs
- The buyer decision to close: Who detects bottle starvation and how should bottle supply and filling equipment respond?
- Current drawings, data and operating records from Approved empty-container or closure supply.
- Approved terminal requirements and failure behavior from The connected handling, rinsing, filling or capping function.
- Project evidence for closure: the starvation-response state map, current drawings, approved supplier data and the agreed witnessed result.
- Named buyer, supplier and local owners for assumptions, actions, review and final approval.
04
Interface Map
One controlled record for the physical, process, utility, control and evidence boundary.
SystemInterfaceCard
Bottle Starvation Control at the Filler
- Upstream system
- Approved empty-container or closure supply
- Downstream system
- The connected handling, rinsing, filling or capping function
- Transferred material
- The project-specific material, state, terminal condition and evidence described by Bottle Starvation Control at the Filler
- Physical connection
- The documented physical, process, utility, signal or evidence boundary covered by this topic.
- Required condition
- The buyer and connected parties approve one current basis for this decision: Who detects bottle starvation and how should bottle supply and filling equipment respond?
- Utility requirement
- Machine and transfer terminal conditions must be taken from the approved bottle, closure and supplier basis for the actual project.
- Control signal
- Availability, ready, hold, stop, fault, reset and restart information as applicable to the boundary
- Failure response
- Bottle Starvation Control at the Filler is treated as agreed even though its condition, owner, revision or evidence remains open. Hold the affected decision or operation until the named owner confirms the recovery basis.
- Evidence required
- Starvation-response state map, supported by the starvation-response state map, current drawings, approved supplier data and the agreed witnessed result.
Equipment Context at This Boundary
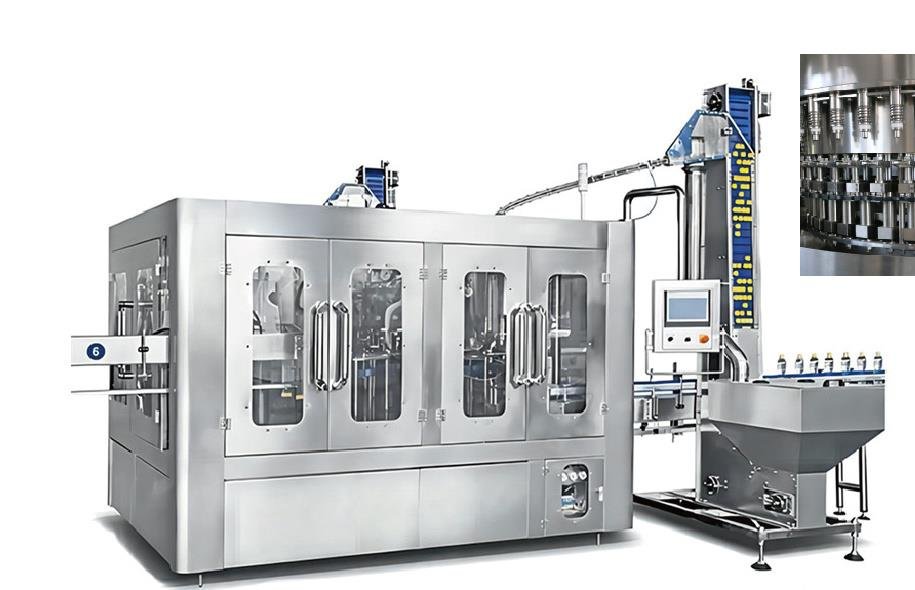
Equipment Used Across This System Scope
These images identify equipment categories and connection points. Final model and configuration selection remains project-specific.
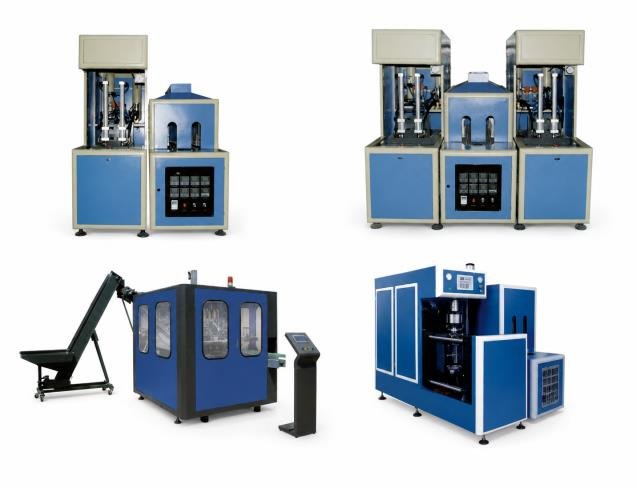
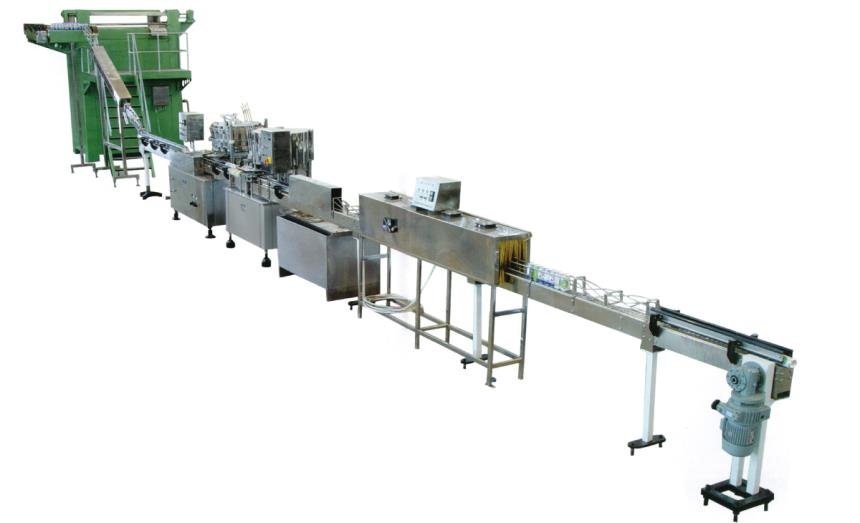
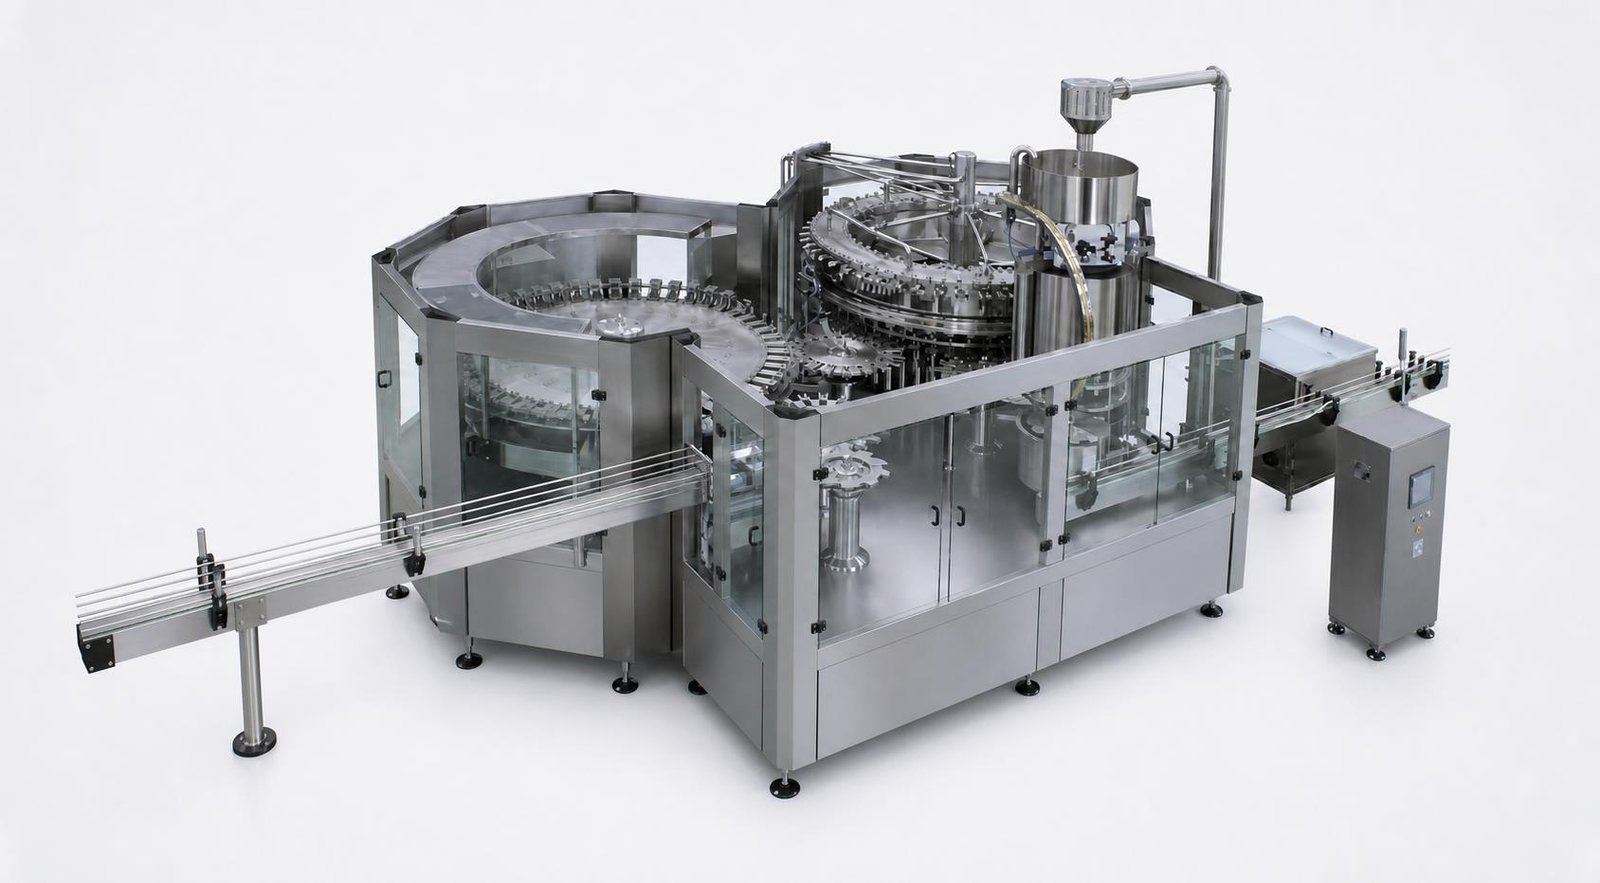
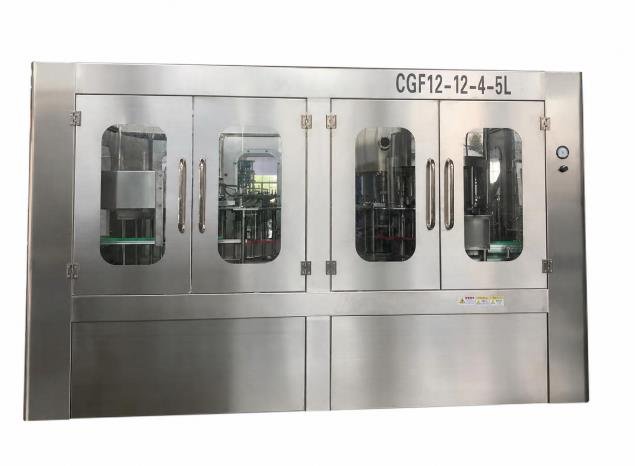
Catalog reference image used to explain equipment and system interfaces. It is not a fixed package or a completed customer project.
05
Main Design Decisions
Decision basis
Assign the detecting sensor or state, delay basis, upstream demand, filler hold or stop response, fault distinction and repeatable restart conditions.
Boundary and handoff
Record The project-specific material, state, terminal condition and evidence described by Bottle Starvation Control at the Filler between Approved empty-container or closure supply and The connected handling, rinsing, filling or capping function.
Required condition and ownership
The buyer and connected parties approve one current basis for this decision: Who detects bottle starvation and how should bottle supply and filling equipment respond?. The buyer approves the reference container and closure; the connected suppliers confirm handling limits, states, change parts and test evidence.
Closure artifact
Maintain the starvation-response state map against the starvation-response state map, current drawings, approved supplier data and the agreed witnessed result and preserve the approved revision.
06
Trade-offs to Resolve
Define now vs. carry an assumption
Closing this decision early can narrow supplier interpretation. Leaving it open may preserve options, but the assumption and later decision gate must be visible.
Local machine simplicity vs. system coordination
A wider format envelope can preserve future options, while increasing handling, change-part and verification scope for the current installation.
Broader scope vs. controlled boundary
It does not select equipment models, publish unsupported performance values or replace project-specific engineering. Keep the page focused on the evidence needed for this one system decision.
07
Common Failure Modes
These are realistic review scenarios, not claims about a completed project.
- Bottle Starvation Control at the Filler is treated as agreed even though its condition, owner, revision or evidence remains open.
- The upstream and downstream parties use different product, format, operating or revision assumptions.
- The required condition is described but no party owns detection, response, reset or approval.
- The interface is accepted from a catalog or nominal value without current project evidence.
- A drawing or successful local machine test is treated as proof of the complete connected behavior.
08
Required Documents
- Starvation-response state map with owner, revision and status
- Approved bottle, neck and closure drawings
- Signed reference samples or sample-control record
- Dimensioned transfer and change-part information
- Connected operating-state and test record
09
Questions to Ask Before Quotation
- Who detects bottle starvation and how should bottle supply and filling equipment respond?
- What exact material, condition, signal, document or decision crosses this boundary?
- Which party detects a missing condition, owns the response and authorizes recovery?
- Which current document, sample, measurement or witnessed result will close the starvation-response state map?
- Which unknown remains open, who must confirm it and before which project decision?
Project-Specific Confirmation
This guide is an engineering interpretation for early coordination. The final starvation-response state map, equipment arrangement, terminal conditions, responsibilities and acceptance criteria require current project data and written approval by the applicable buyer, suppliers and local responsible parties.
11
Related System Pages
Questions
Questions About This Interface Decision
Does bottle starvation prove the blower is too small?
No. A persistent demonstrated supply deficit differs from transfer loss, rejected bottles or receiving-permission failure. Compare the same approved format and interval before attributing the loss to source capacity.
Can the filler be starved while bottles are visible upstream?
Yes, an upstream stock picture does not prove usable delivery at the receiving point. Preserve the transfer sequence, format identity and signal meanings to locate where accepted supply stops; qualified personnel must use approved safe inspection methods.
Should I increase blower speed or air-conveyor airflow?
Not from the waiting message alone. Those settings depend on the approved bottle, transfer design and supplier limits. First identify the missing condition and responsible interface; this guide cannot authorize a safe adjustment.
Is a standard machine-state name enough for mixed vendors?
No. Even a shared label needs the actual source, meaning, response and receiving permission agreed. Application-specific transition logic and safety functions cannot be inferred from a label or from this planning page.
What should a supplier show after a proposed change?
Evidence on the same bottle, conditions, observation interval and good-output boundary, with shortage events and restart results traceable. Keep unresolved events visible. Allot Tech can coordinate responsibilities, not certify unseen equipment or guarantee a production gain.
Turn the unknowns into a reviewable interface
Review This System Decision
Share the available bottle, output, site, utility and supplier evidence. Open items can remain explicitly marked for confirmation.