
System Planning and Definition
Water Bottling System FAT & SAT: From Factory Pass to Site Acceptance
FAT passed but the installed water bottling system still stops? Plan real interface checks, site prerequisites and deviation retests before accepting the line.
Decision focus
Which factory evidence can you rely on, and which connected-system checks remain open at your site?
01
Direct Answer
A factory pass proves only the documented equipment, format and conditions tested. Site acceptance must address the actual utilities, bottle transfers, connected-machine signals and agreed output basis. Identify simulations and absent equipment explicitly; resolve open prerequisites and deviations against an agreed test plan, not a shipment date.
FAT passed. Why is the installed system not ready for acceptance?
Separate a failed result from an untested connection or a missing prerequisite. Start with the acceptance record and the boundary it actually covered.
Map what was tested and what was simulated
List the machines physically connected during FAT, absent downstream equipment and simulated ready/blocked signals. Record reference bottles, caps, labels, drawings and software revisions. For each requirement, name the test method, acceptance criterion and evidence to be completed on site. A substituted bottle or simulated packer does not demonstrate every contracted format or the installed line.
Trace the installed interface, not just the filler speed
If the packer stops and bottles accumulate, compare time-aligned filler, conveyor and packer states with the agreed handshakes. Check the defined utility conditions at the relevant machine inlet under the documented operating condition. A static pressure photograph or matching PLC brand does not establish connected operation. Any restart or abnormal-state test must follow an approved procedure led by qualified personnel; never bypass safeguards.
Close deviations with repeatable evidence
Record the requirement, observed condition, test setup, result, limitation, impact and responsible owner. Agree the corrective action and retest basis before closing the issue. If a software revision or format part changes, identify the affected scenarios for repeat testing. A missing site connection is an open prerequisite, not a passed test; contractual release and acceptance decisions remain with the authorized project parties.
Close open test items with evidence rather than a status label
Keep each unresolved FAT or SAT item tied to the requirement, observed result, affected boundary, responsible party and evidence needed for closure. Record what was not tested and why; an entry marked completed is not a substitute for the agreed record. If hardware, software, materials or settings change after a test, qualified reviewers must decide which earlier results remain applicable and which connected checks need repeating. Separate permission to ship or install from acceptance of installed performance. A video can support an observation only within its stated bottle, operating condition and recording period; it cannot establish every interface or replace missing site evidence.
Prepare before the site acceptance review
- Agree the test boundary, formats, method and project-specific acceptance criteria.
- Mark each interface as physically tested, simulated, absent or still awaiting verification.
- Bring controlled drawings, software revisions, trial materials and relevant site-condition records.
- Keep a deviation register with owners, retest evidence and the applicable handover decision.
- List open items with requirement references, closure evidence, change impact and an agreed review owner.
Planning guidance, not project acceptance approval. Allot Tech can help organize buyer–supplier clarification; the project team must approve the test procedure, safe conditions and acceptance decisions.
Resolve the connected questions
- Check site utilities — Define inlet conditions and connection responsibilities before interpreting a test.
- Set the accepted-output basis — Distinguish filler readings from accepted output at the agreed system boundary.
- Review blocked-state coordination — Clarify what upstream machines should do when downstream equipment cannot receive bottles.
Planning essentials
What Should Water Bottling System FAT and SAT Prove?
A practical answer for buyers comparing equipment, scope and connected-system requirements.
The first question is the tested boundary. A successful test of a filling machine is not evidence that an absent labeler, packer or existing conveyor will work with it. State which equipment is physically connected, which signals are simulated and which site-dependent checks remain open.
Prepare controlled reference materials: bottles, caps, labels and packs relevant to the agreed scope. Record their revisions and any substitution. A test with a substitute container can be informative, but the record should not silently treat it as proof for the final commercial format.
Acceptance criteria, test durations, allowed deviations and release decisions belong in the agreed project documents. This checklist does not set universal values. Any stop, fault or recovery scenario must follow the approved safe test procedure and be carried out by authorized personnel; do not bypass protective controls to complete a checklist.
Factory-verifiable
Inspect machine functions, documents, terminals and credible simulations that exist before shipment.
Site-dependent
Verify installed utilities, physical transfers, networks, mixed-vendor behavior and site recovery.
Scenario-based
Test normal flow plus agreed shortage, blockage, fault, stop and restart conditions.
Evidence-controlled
Record prerequisites, reference materials, observations, results, deviations, owners and retest status.
System scope
Water Bottling System FAT-to-SAT Evidence Matrix
Assign each interface claim to the earliest credible test condition.
Scroll the table sideways to read every column. With a keyboard, focus the table and use the left or right arrow key.
| Evidence area | FAT scope where available | SAT or connected-site scope |
|---|---|---|
| Documents and terminals | Verify current drawings, lists, labels and accessible machine terminals. | Confirm installed revision, connection and as-built record. |
| Material transfer | Use approved samples or a documented simulation when the adjacent machine is absent. | Observe connected product, bottle, cap or pack transfer under agreed conditions. |
| Utilities | Verify machine-side requirements, monitoring and simulated loss response where practical. | Measure available terminal conditions and witness permissive or recovery behavior. |
| States and signals | Simulate ready, demand, blocked, starved, fault, reset and restart exchanges. | Verify meanings and timing across the installed connected machines. |
| Normal production | Test the available machine or assembled scope on the stated reference basis. | Run the installed connected scope under the approved product and format basis. |
| Deviation closure | Record unresolved factory findings, owner and site prerequisite. | Retest applicable items and close or formally disposition remaining deviations. |
Compare the options
What Belongs in a Traceable Acceptance Test Record?
A result should identify exactly what was demonstrated. An open item needs an owner and a defined next test.
Scroll the table sideways to read every column. With a keyboard, focus the table and use the left or right arrow key.
| Record field | What to write | Avoid this ambiguity |
|---|---|---|
| Requirement and setup | Requirement ID, equipment boundary, software/drawing revisions and connected or simulated interfaces. | Passed without naming the tested configuration. |
| Reference materials | Bottle, cap, label and pack identity; note substitutions or excluded formats. | Assuming one tested bottle proves all offered formats. |
| Conditions and method | Available utilities, operating state, approved duration and measurement method. | Comparing a momentary machine speed with sustained packed output. |
| Observed result | Actual observations and agreed output, reject and interruption records where applicable. | Only recording the control-screen setpoint. |
| Deviation and disposition | Issue, affected requirement, responsible party, action, retest evidence and approval status. | Closing a site-dependent issue solely because shipment is scheduled. |
Practical review
Acceptance Example: The Packer Is Not Available at FAT
Hypothetical test-planning example, not a record of completed equipment testing.
Scroll the table sideways to read every column. With a keyboard, focus the table and use the left or right arrow key.
| Claim to examine | Factory evidence possible | Site evidence still required |
|---|---|---|
| Filler discharge behavior | The available machine and approved local discharge setup, with limitations recorded. | Physical transfer to the installed downstream equipment. |
| Blocked/ready signal meaning | An agreed simulation can exercise the defined signal behavior. | End-to-end meaning and response with the actual packer and conveyor controls. |
| Saleable packed output | Do not claim a complete packed-output result from the filler test alone. | The agreed connected run using the specified bottle and pack. |
| Deviation closure | Record the missing equipment and the open verification actions. | Named parties review site evidence and approve the required disposition. |
An honest FAT report can contain open SAT actions. The important distinction is between evidence already obtained and a test that still depends on the installed site.
Choose Your Next Planning Step
Test prerequisites lack confirmed site services?
Confirm utility requirements firstNeed to align the output measurement basis?
Compare the saleable-output basisThe test includes retained equipment?
Prepare the existing-line survey
02
Position in the System
This guide focuses on integrated-interface evidence and not contractual handover or generic machine inspection. It controls the boundary between Buyer requirements, approved product formats and available site records and A coordinated mixed-vendor system definition for technical review. It assumes no universal test duration, performance threshold or contractual acceptance process.
03
Buyer Inputs
- The buyer decision to close: Which connected-interface scenarios can be verified before shipment and which require the installed site condition?
- Current drawings, data and operating records from Buyer requirements, approved product formats and available site records.
- Approved terminal requirements and failure behavior from A coordinated mixed-vendor system definition for technical review.
- Project evidence for closure: approved test protocols, interface matrices, reference samples, results and deviation records.
- Named buyer, supplier and local owners for assumptions, actions, review and final approval.
04
Interface Map
One controlled record for the physical, process, utility, control and evidence boundary.
SystemInterfaceCard
Water Bottling System FAT and SAT for Connected Interfaces
- Upstream system
- Buyer requirements, approved product formats and available site records
- Downstream system
- A coordinated mixed-vendor system definition for technical review
- Transferred material
- Test scenarios, prerequisites, simulations, site dependencies, results and open deviations
- Physical connection
- The documented physical, process, utility, signal or evidence boundary covered by this topic.
- Required condition
- Every acceptance claim references an agreed scenario, reference format, prerequisite and disposition rule
- Utility requirement
- Only equipment terminal conditions are recorded here; plant distribution and local code design remain with the responsible local parties.
- Control signal
- Availability, ready, hold, stop, fault, reset and restart information as applicable to the boundary
- Failure response
- A factory test is treated as proof of a site interface that was not physically available or credibly simulated. Hold the affected decision or operation until the named owner confirms the recovery basis.
- Evidence required
- Interface FAT-to-SAT evidence matrix, supported by approved test protocols, interface matrices, reference samples, results and deviation records.
Equipment Context at This Boundary
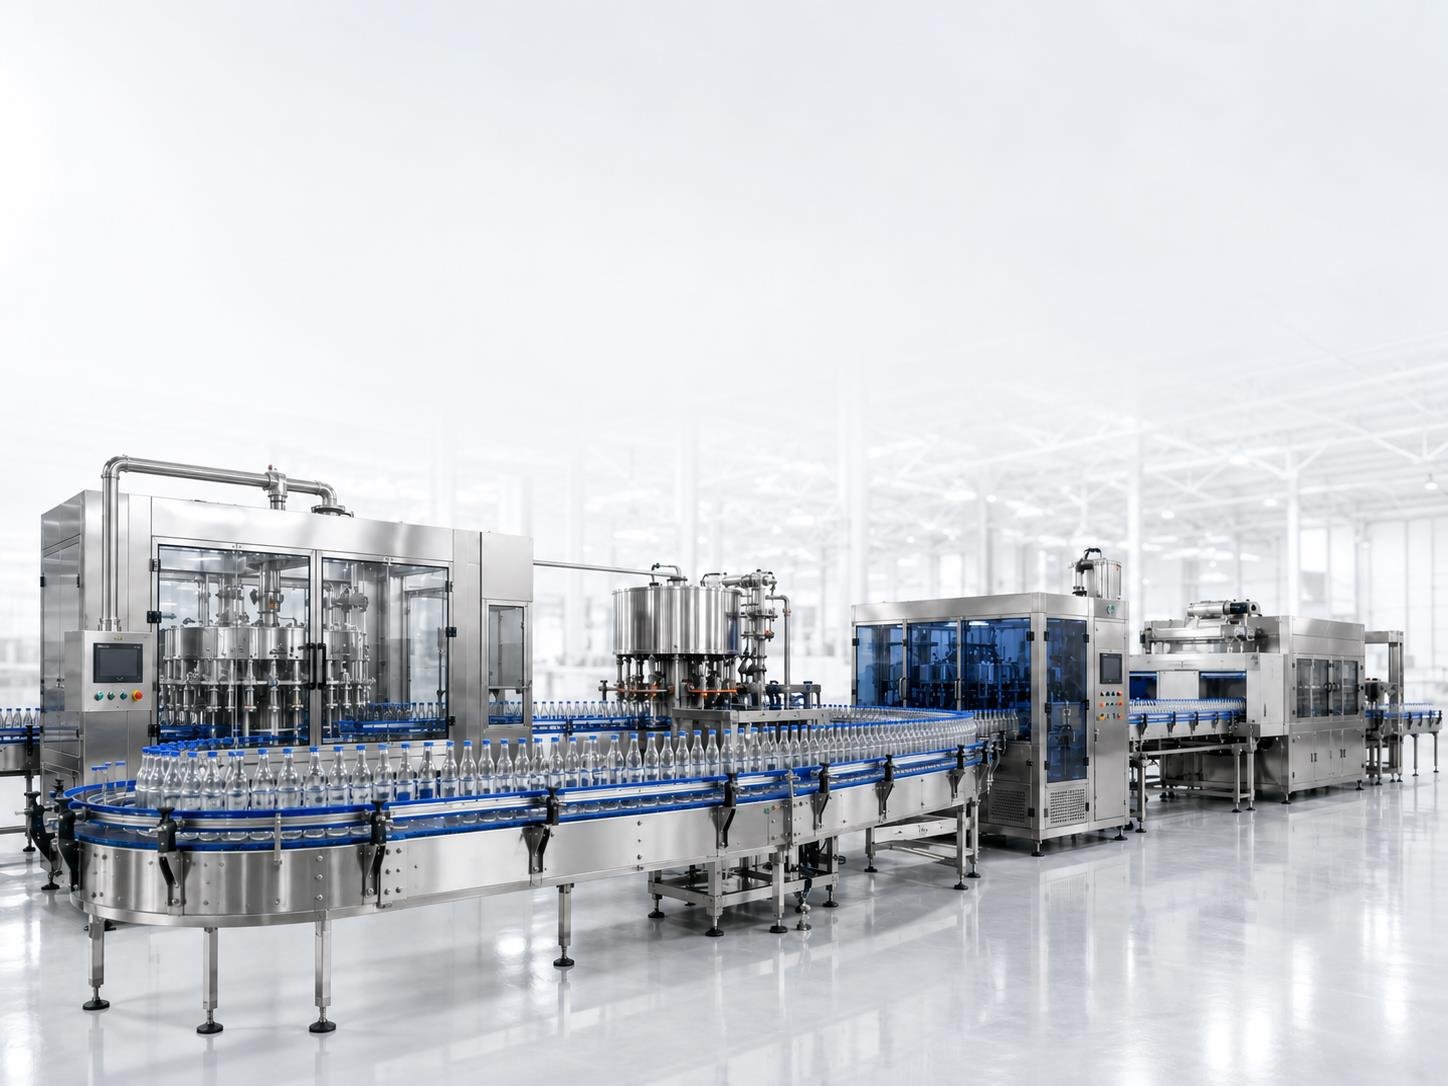
Equipment Used Across This System Scope
These images identify equipment categories and connection points. Final model and configuration selection remains project-specific.
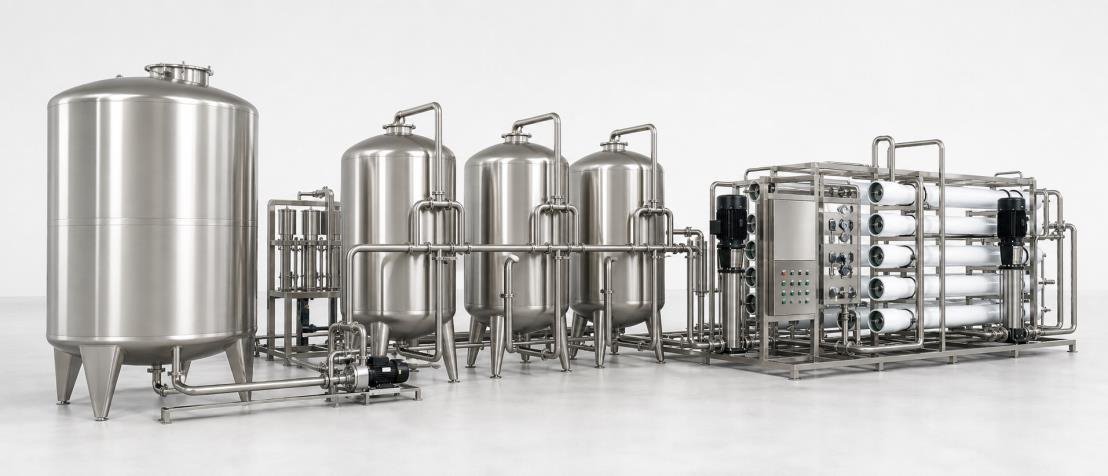
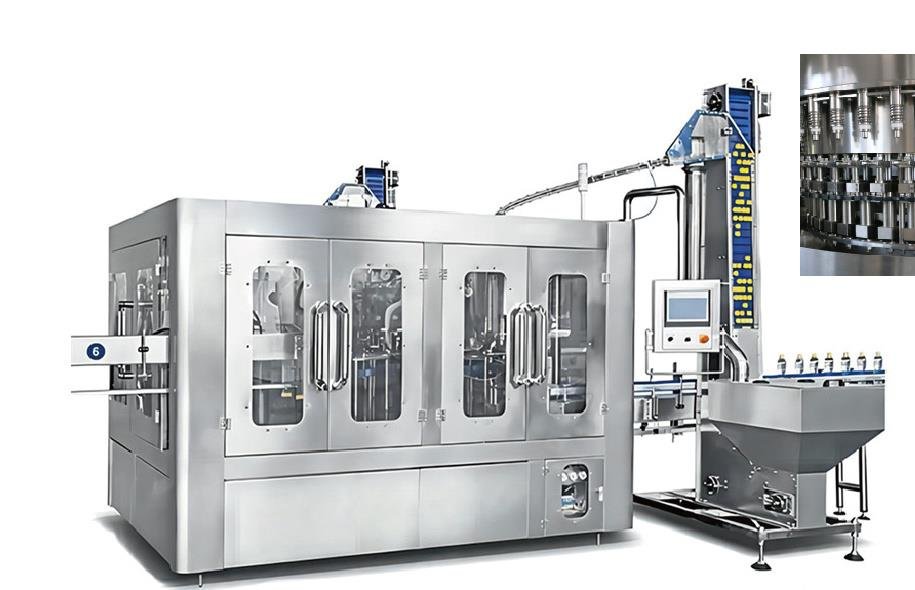
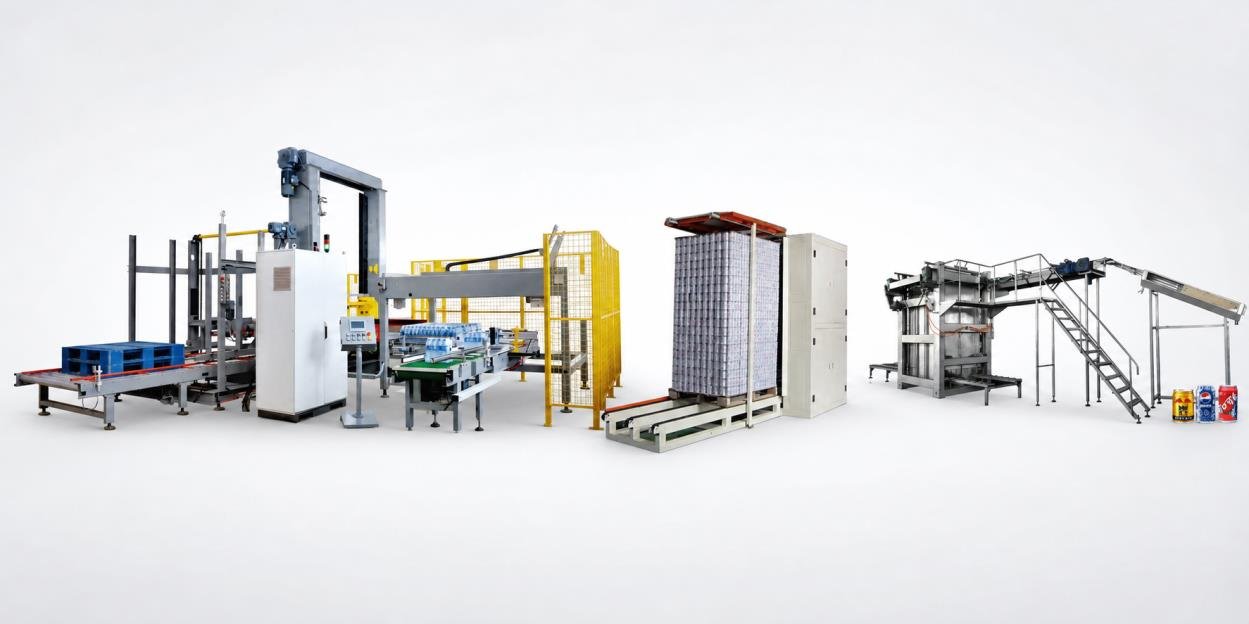
Catalog reference image used to explain equipment and system interfaces. It is not a fixed package or a completed customer project.
05
Main Design Decisions
Decision basis
Separate factory-verifiable machine and simulated handshake evidence from site-dependent utility, transfer, communications, stop-recovery and integrated-run evidence, then assign prerequisites and acceptance criteria to each.
Boundary and handoff
Record Test scenarios, prerequisites, simulations, site dependencies, results and open deviations between Buyer requirements, approved product formats and available site records and A coordinated mixed-vendor system definition for technical review.
Required condition and ownership
Every acceptance claim references an agreed scenario, reference format, prerequisite and disposition rule. The buyer owns the operating requirement; each supplier owns its machine data; the system coordinator maintains the shared interface record.
Closure artifact
Maintain the interface FAT-to-SAT evidence matrix against approved test protocols, interface matrices, reference samples, results and deviation records and preserve the approved revision.
06
Trade-offs to Resolve
Define now vs. carry an assumption
Closing this decision early can narrow supplier interpretation. Leaving it open may preserve options, but the assumption and later decision gate must be visible.
Local machine simplicity vs. system coordination
A broader early definition can expose more gaps, while a narrower definition can move decisions faster. The chosen boundary must remain explicit.
Broader scope vs. controlled boundary
It assumes no universal test duration, performance threshold or contractual acceptance process. Keep the page focused on the evidence needed for this one system decision.
07
Common Failure Modes
These are realistic review scenarios, not claims about a completed project.
- A factory test is treated as proof of a site interface that was not physically available or credibly simulated.
- The upstream and downstream parties use different product, format, operating or revision assumptions.
- The required condition is described but no party owns detection, response, reset or approval.
- The interface is accepted from a catalog or nominal value without current project evidence.
- A drawing or successful local machine test is treated as proof of the complete connected behavior.
08
Required Documents
- Interface FAT-to-SAT evidence matrix with owner, revision and status
- Approved design-basis register
- Current equipment and interface list
- Open-input and decision log
- Revision-controlled supplier data
09
Questions to Ask Before Quotation
- Which connected-interface scenarios can be verified before shipment and which require the installed site condition?
- What exact material, condition, signal, document or decision crosses this boundary?
- Which party detects a missing condition, owns the response and authorizes recovery?
- Which current document, sample, measurement or witnessed result will close the interface FAT-to-SAT evidence matrix?
- Which unknown remains open, who must confirm it and before which project decision?
Project-Specific Confirmation
This guide is an engineering interpretation for early coordination. The final interface FAT-to-SAT evidence matrix, equipment arrangement, terminal conditions, responsibilities and acceptance criteria require current project data and written approval by the applicable buyer, suppliers and local responsible parties.
11
Related System Pages
Questions
Questions About This Interface Decision
Does a passed FAT remove the need for SAT?
No. FAT may cover only the factory configuration. SAT addresses the installed interfaces and site conditions that were absent or simulated; use the agreed project test scope.
Can substitute bottles prove all production formats?
No. Record the substitution and its limitations. The responsible parties must specify which actual formats and related parts require later verification.
How long should a bottling system acceptance test run?
There is no universal duration. Agree the operating conditions, observation period, output boundary and acceptable deviations for the project before testing.
What if a connection or retest record is missing?
Mark the requirement unresolved, assign an owner and define the evidence still needed. Do not relabel missing evidence as a pass; use the project's authorized review process.
Does a shipment release mean the connected line has passed SAT?
No. Shipment and site acceptance address different conditions. Record the factory-tested scope, remaining site connections and open items, then use the agreed installed-system criteria. Do not infer SAT completion from dispatch documents, a machine video or an unchecked status field.
Turn the unknowns into a reviewable interface
Build My FAT/SAT Test Basis
Share the available bottle, output, site, utility and supplier evidence. Open items can remain explicitly marked for confirmation.