
System Planning and Definition
Water Bottling System Capacity: Diagnose the Interface Bottleneck
Find why the bottling line misses its finished-output target. Compare stage duties fairly, trace interruptions and prepare evidence for a connected capacity test.
Decision focus
Which verified stage or operating condition limits good finished output?
01
Direct Answer
Compare water bottling system capacity from a common bottle, pack and production period, not the largest machine rating. Convert each confirmed stage duty to bottles per hour, record missing inputs and compare actual good packs at the line exit. Then trace waiting, blockage and recovery events before proposing more equipment.
Diagnose low output before increasing the line speed
If the filler counter meets its target but dispatch receives fewer good packs, first check where and when the two counts were taken. Stock held on conveyors, rejected bottles, incomplete packs and different observation periods can make the numbers incomparable. Set one counting boundary before calling the difference a capacity fault.
Put water, bottles and packs on the same hourly basis
Record bottle volume, bottles per pack and the operating conditions behind each supplier rate. Net product water in L/h divided by L/bottle gives a water-supply equivalent in bottles/h. Packing in packs/minute multiplied by bottles/pack and by 60 gives a bottle equivalent. This arithmetic does not confirm that either stage can sustain its quoted duty. Keep cleaning, rinsing and other water demands separate; a raw-water or pump rating is not net product water available at filling.
Use stop chronology to distinguish shortage from blockage
A starved machine is waiting for upstream material or an agreed release condition; a blocked machine cannot discharge to the next stage. Record the first event, its timestamp and the states of neighboring machines, alongside faults and replenishment. A filler stopping after packing stops may be responding correctly to a downstream block. Review bottle transfer, label or film supply, pack removal and utility conditions before blaming filler speed. Do not add overlapping machine stop durations as if they were separate lost production periods.
Check recovery and finished output, not just running speed
The lowest comparable confirmed duty is a preliminary ceiling for the listed stages, not guaranteed saleable production. An accumulator may cover a temporary mismatch but cannot remove a sustained downstream rate deficit. Agree how the buffer clears and how the line returns to stable output after representative stops. Measure accepted finished packs over a stated period with the reference bottle, materials, utilities and changeover scope recorded. Keep availability and reject allowances project-specific; do not insert a default OEE.
Avoid counting the same production loss several times
Keep one line-level observation interval alongside the individual machine records. If packing blocks, the filler stops and bottle supply then waits, those overlapping stop durations are not three separate periods of lost line production. Mark the first observed event and the connected responses without assuming that the first alarm is the root cause. Reconcile good finished packs with rejects and changes in stock held between the chosen counting boundaries. Record planned cleaning and format changes explicitly so a running-speed comparison is not presented as a whole-shift result. The worksheet converts entered rates; it does not reconstruct these losses or predict an operating efficiency.
Build a useful capacity review record
- Reference bottle drawing and fill volume, cap, label, pack collation and counting point.
- Supplier duties with units, format, conditions and document revisions; unconfirmed values marked open.
- Time-aligned machine states, good finished counts, rejects, replenishment and planned interruptions.
- Connected test period, acceptance criteria, recovery scenarios and responsibility for unresolved inputs.
- Keep a line-level timeline with overlapping stops, counting boundaries and opening/closing work-in-process stock.
Planning guidance only. Unit conversion does not approve a machine selection or promise output. Qualified personnel must agree safe observation and testing; never bypass guards or change safety settings to reach a target.
Investigate the connected cause
- Check the machine utility supply — Compare conditions at the power, air and water connection during demand.
- Review conveyor accumulation — Separate temporary stop protection from sustained processing capacity.
- Decide what to upgrade — Connect the measured constraint to a complete retrofit scope.
Planning essentials
How to Choose Water Bottling System Capacity on a Comparable Basis
A practical answer for buyers comparing equipment, scope and connected-system requirements.
Capacity should be tied to a reference bottle, saleable unit and operating period. Treatment output, bottle supply, filling, labeling, packing and recovery performance cannot be compared when suppliers quote different products, container sizes or time bases.
The preliminary system rate follows the lowest confirmed sustainable duty on the same basis, subject to the buyer operating schedule and any project-approved allowances. Missing values remain open; this page does not insert assumed efficiency, yield or availability factors.
Normalize the unit
State bottles, liters, packs or pallets per period and the exact reference format.
Separate rated and sustainable duty
Ask each supplier which product, format and operating conditions support the stated rate.
Include interruptions
Record changeovers, cleaning, material replenishment and planned operating windows as buyer inputs.
Keep unknowns visible
Do not manufacture a final answer when one module or operating assumption is not confirmed.
System scope
Water Bottling System Capacity Comparison Chain
Compare every module against the same reference bottle and time basis.
Scroll the table sideways to read every column. With a keyboard, focus the table and use the left or right arrow key.
| Capacity point | Required comparison basis | Evidence to request |
|---|---|---|
| Treated-water supply | Usable supply for the stated product and operating period. | Treatment net-output basis, storage and transfer schedule. |
| Bottle supply | Approved container delivered in the required condition. | Blower or feeding duty, format basis and bottle-release record. |
| Filling and closure | Sustainable saleable output on the reference bottle and cap. | Supplier duty statement, product basis and applicable trial evidence. |
| Labeling and coding | Accepted labeled and coded bottles on the same format basis. | Material specification, changeover basis and reject conditions. |
| Secondary packing | Accepted finished packs using the agreed collation and material. | Pack drawing, film or carton basis and sustainable duty. |
| Connected recovery | Return to stable production after agreed shortage, blockage and fault scenarios. | State matrix, event evidence and witnessed connected-run record. |
Practical review
Worked Example: Convert Every Module to Bottles per Hour
Illustrative arithmetic only, not an Allot Tech model rating or project result. Suppose the reference bottle is 0.5 L and the pack contains 12 bottles. All five input rates below are assumed to be sustainable on that same basis.
Scroll the table sideways to read every column. With a keyboard, focus the table and use the left or right arrow key.
| Module | Illustrative input and calculation | Comparable rate |
|---|---|---|
| Net product-water supply | 6,000 L/h divided by 0.5 L/bottle | 12,000 bottles/h |
| Approved bottle supply | 12,000 bottles/h, already on the reference-bottle basis | 12,000 bottles/h |
| Filling and capping | 10,000 bottles/h on the same bottle and cap | 10,000 bottles/h |
| Labeling and coding | 11,000 bottles/h with the specified material and code | 11,000 bottles/h |
| Secondary packing | 12 packs/minute multiplied by 12 bottles/pack multiplied by 60 | 8,640 bottles/h |
Packing is the lowest listed duty at 8,640 bottles/h. This is a screening ceiling from the five inputs, not guaranteed connected output. Moving packing to 15 packs/minute gives 10,800 bottles/h at that stage, so the lowest listed duty becomes filling at 10,000 bottles/h. Neither result includes unlisted stages, rejects, interruptions, cleaning or changeovers. Use net water available for product filling after separately accounting for rinsing, losses and other demands.
Your rate comparison
Water Bottling System Capacity Worksheet
Convert five stage duties to bottles per hour. Use sustainable rates for one bottle, cap, product and pack basis. The lowest listed duty is a screening ceiling, not promised output.
Leave unknown values blank. Water input means net product water available for filling after other demands are accounted for. This calculation covers only the five listed stages; it adds no assumed efficiency, yield or operating time. Values stay in this page and are not submitted or saved.
Next, record unlisted conveyor, inspection, pallet, utility and recovery constraints in the interface gap checklist, then request a system review with supplier duty sheets.
02
Position in the System
This guide creates a user-input constraint chain for interface review, not a universal BPH calculator. It controls the boundary between Buyer requirements, approved product formats and available site records and A coordinated mixed-vendor system definition for technical review. It publishes no default efficiency, OEE, buffer duration, BPH band or guaranteed capacity.
03
Buyer Inputs
- The buyer decision to close: Which confirmed machine, material, utility, schedule or recovery condition constrains the requested saleable output?
- Current drawings, data and operating records from Buyer requirements, approved product formats and available site records.
- Approved terminal requirements and failure behavior from A coordinated mixed-vendor system definition for technical review.
- Project evidence for closure: approved supplier duties, buyer schedule, actual operating records and stated unknowns.
- Named buyer, supplier and local owners for assumptions, actions, review and final approval.
04
Interface Map
One controlled record for the physical, process, utility, control and evidence boundary.
SystemInterfaceCard
Water Bottling System Capacity Constraint Register
- Upstream system
- Buyer requirements, approved product formats and available site records
- Downstream system
- A coordinated mixed-vendor system definition for technical review
- Transferred material
- Confirmed sustainable duties, operating assumptions, interruptions and unresolved constraints
- Physical connection
- The documented physical, process, utility, signal or evidence boundary covered by this topic.
- Required condition
- All compared values use the same reference format, time basis and stated operating condition
- Utility requirement
- Only equipment terminal conditions are recorded here; plant distribution and local code design remain with the responsible local parties.
- Control signal
- Availability, ready, hold, stop, fault, reset and restart information as applicable to the boundary
- Failure response
- Nominal values stated on different bases are combined into a false system output. Hold the affected decision or operation until the named owner confirms the recovery basis.
- Evidence required
- Capacity constraint and missing-data register, supported by approved supplier duties, buyer schedule, actual operating records and stated unknowns.
Equipment Context at This Boundary
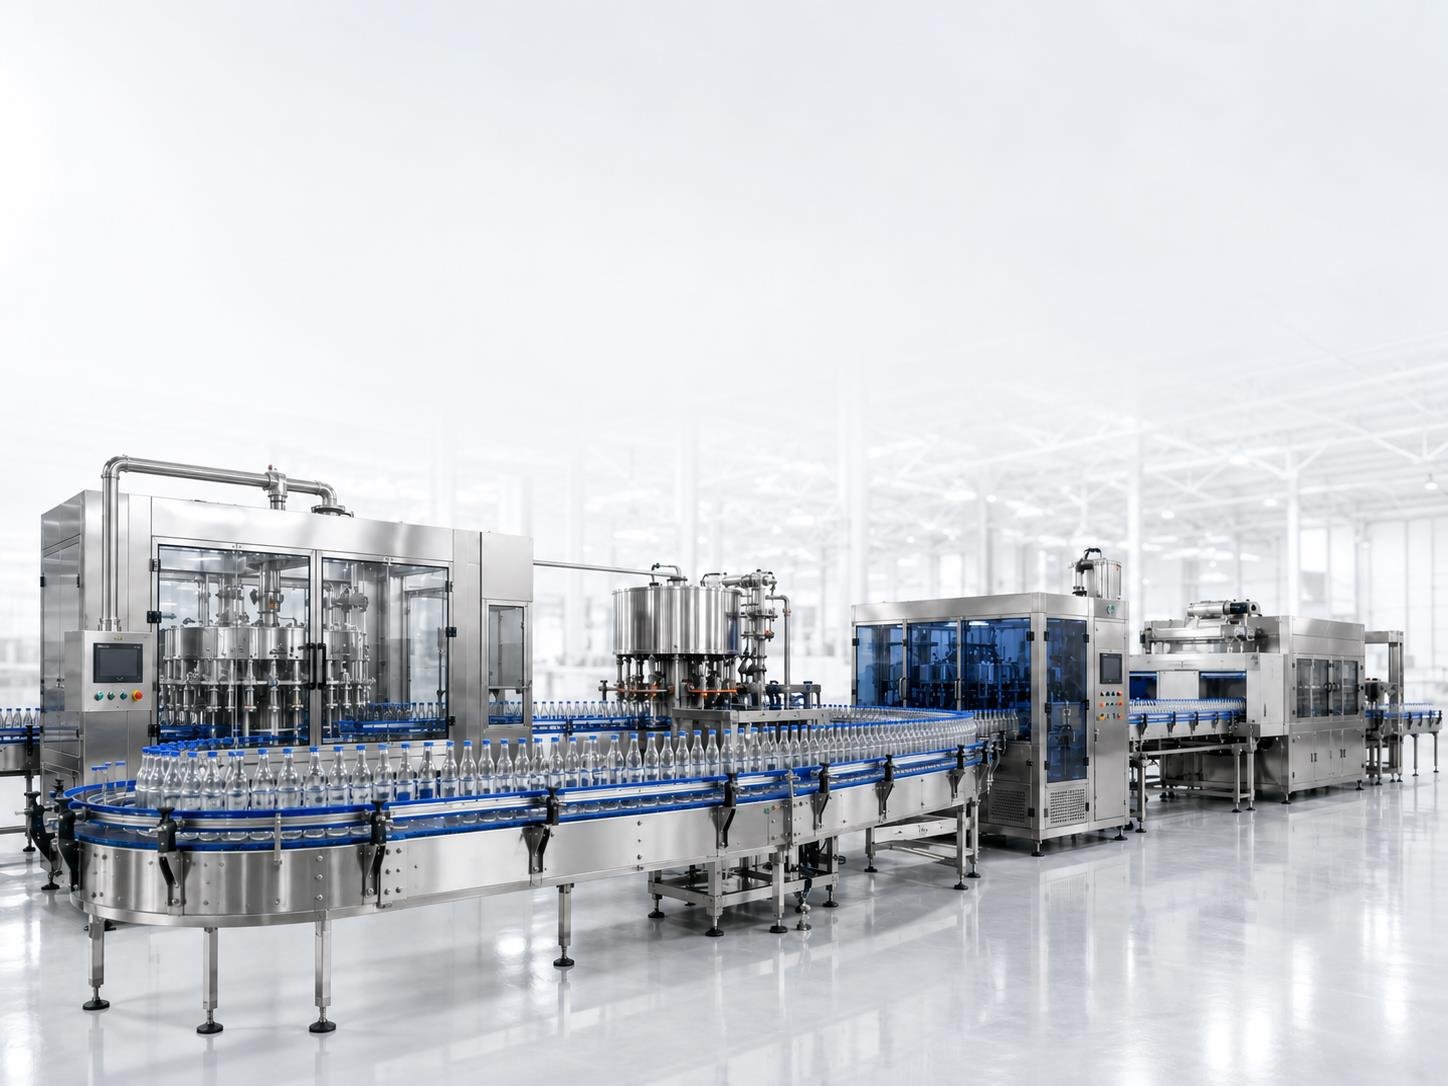
Equipment Used Across This System Scope
These images identify equipment categories and connection points. Final model and configuration selection remains project-specific.
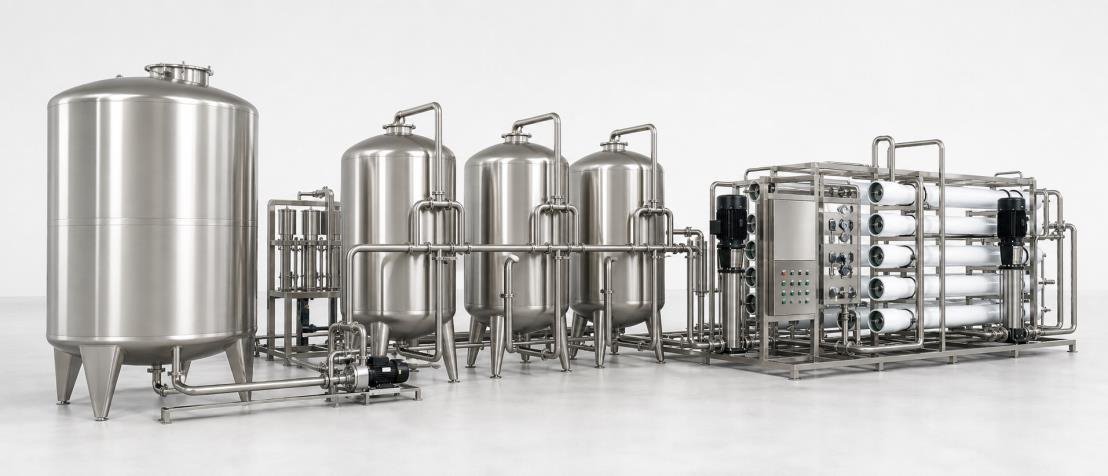
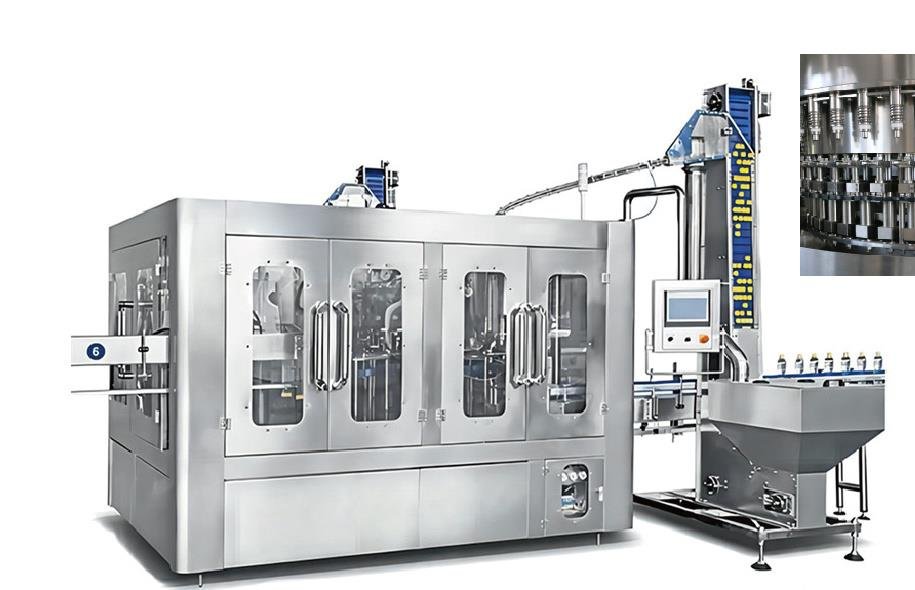
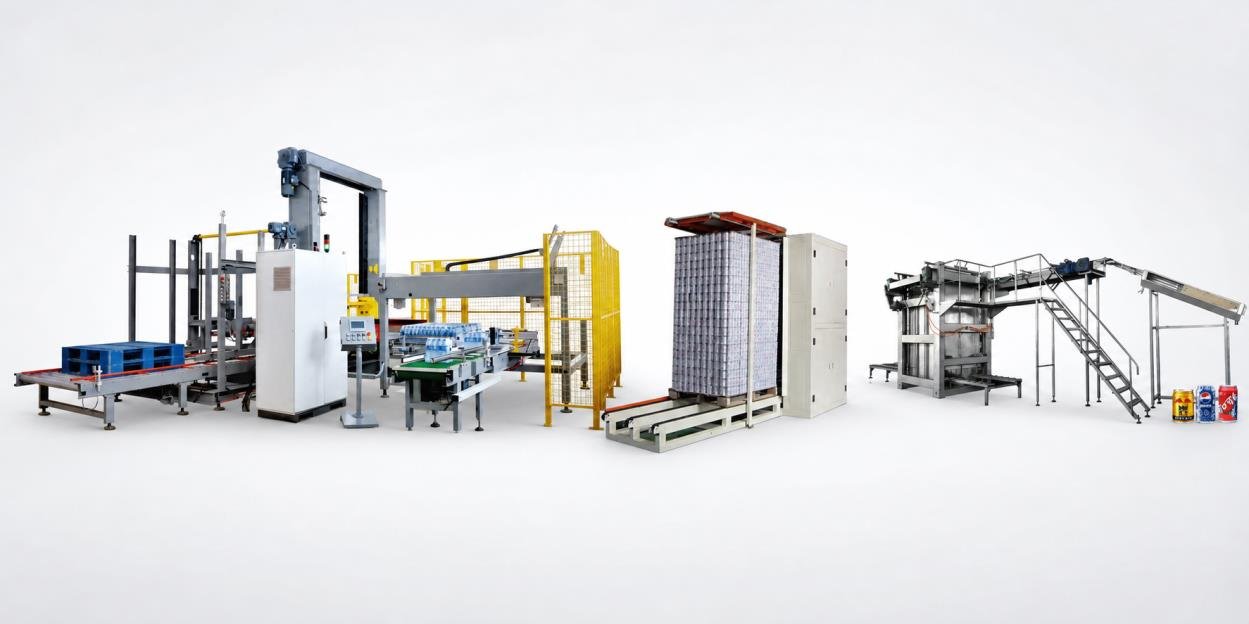
Catalog reference image used to explain equipment and system interfaces. It is not a fixed package or a completed customer project.
05
Main Design Decisions
Decision basis
Capacity balance should compare only confirmed duties on one bottle, product and operating basis, then show missing data and constraints without inserting assumed efficiencies or promising a final output.
Boundary and handoff
Record Confirmed sustainable duties, operating assumptions, interruptions and unresolved constraints between Buyer requirements, approved product formats and available site records and A coordinated mixed-vendor system definition for technical review.
Required condition and ownership
All compared values use the same reference format, time basis and stated operating condition. The buyer owns the operating requirement; each supplier owns its machine data; the system coordinator maintains the shared interface record.
Closure artifact
Maintain the capacity constraint and missing-data register against approved supplier duties, buyer schedule, actual operating records and stated unknowns and preserve the approved revision.
06
Trade-offs to Resolve
Define now vs. carry an assumption
Closing this decision early can narrow supplier interpretation. Leaving it open may preserve options, but the assumption and later decision gate must be visible.
Local machine simplicity vs. system coordination
A broader early definition can expose more gaps, while a narrower definition can move decisions faster. The chosen boundary must remain explicit.
Broader scope vs. controlled boundary
It publishes no default efficiency, OEE, buffer duration, BPH band or guaranteed capacity. Keep the page focused on the evidence needed for this one system decision.
07
Common Failure Modes
These are realistic review scenarios, not claims about a completed project.
- Nominal values stated on different bases are combined into a false system output.
- The upstream and downstream parties use different product, format, operating or revision assumptions.
- The required condition is described but no party owns detection, response, reset or approval.
- The interface is accepted from a catalog or nominal value without current project evidence.
- A drawing or successful local machine test is treated as proof of the complete connected behavior.
08
Required Documents
- Capacity constraint and missing-data register with owner, revision and status
- Approved design-basis register
- Current equipment and interface list
- Open-input and decision log
- Revision-controlled supplier data
09
Questions to Ask Before Quotation
- Which confirmed machine, material, utility, schedule or recovery condition constrains the requested saleable output?
- What exact material, condition, signal, document or decision crosses this boundary?
- Which party detects a missing condition, owns the response and authorizes recovery?
- Which current document, sample, measurement or witnessed result will close the capacity constraint and missing-data register?
- Which unknown remains open, who must confirm it and before which project decision?
Project-Specific Confirmation
This guide is an engineering interpretation for early coordination. The final capacity constraint and missing-data register, equipment arrangement, terminal conditions, responsibilities and acceptance criteria require current project data and written approval by the applicable buyer, suppliers and local responsible parties.
11
Related System Pages
Questions
Questions About This Interface Decision
Can a bottles/hour rating tell me daily saleable output?
Not alone. State the scheduled period, bottle and pack basis, actual interruptions and accepted finished count. A running-speed rating does not include every stop, changeover or rejected unit.
How do I compare packs/minute with bottles/hour?
Multiply packs/minute by the confirmed bottles/pack and by 60. The result is a common unit for comparison, not evidence of sustained operation or a guaranteed line output.
Will a bigger buffer fix a slow packing machine?
Not a permanent rate deficit. A reviewed buffer can provide temporary space during defined interruptions, but the packer must process the required duty and recover accumulated product under the agreed conditions.
What if one supplier cannot confirm its sustainable capacity?
Keep that stage unresolved. Request the reference format, materials, utility conditions and relevant test evidence. Do not fill the gap with a catalog maximum or multiply the incomplete chain into a production promise.
Why do machine stop totals exceed the observed line stoppage?
Several machines can stop during the same event, so their intervals overlap. Compare timestamps on one line timeline and distinguish the initiating condition from propagated waiting or blockage. Adding every machine duration would count some lost time more than once.
Turn the unknowns into a reviewable interface
Check My Capacity Basis
Share the available bottle, output, site, utility and supplier evidence. Open items can remain explicitly marked for confirmation.